INDUSTRIAL METHODOLOGY & OPERATIONAL QUALITY CONTROL
Large-scale defense fulfillment requires absolute mechanical reproducibility. Our production infrastructure utilizes advanced, closed-loop industrial engineering to guarantee that every single sachet delivered to the theater matches our exact molecular and physical performance benchmarks.
- Continuous Automated Blending Moat: Our production floor utilizes high-capacity, continuous matrix blending systems rather than legacy batch-processing lines. This automated isolation architecture ensures a completely uniform distribution of our bio-protein and mineral matrix across millions of units, maintaining identical compound density from the first sachet to the last.
- Traceable Ingredient Firewalls: We operate a zero-trust raw material procurement protocol. Every cargo lot of natural honey binder, fruit performance compounds, and macro-nutrients entering our facility is immediately locked in quarantine until it clears independent mass spectrometry testing to certify the absolute absence of heavy metals, pesticides, or synthetic contaminants.
- Environmental Packaging Shield: Our localized automated packaging lines wrap the formula inside ruggedized, tri-laminated barrier sachets under a modified nitrogen atmosphere. This technical process eliminates oxygen degradation at the line source, providing the unyielding environmental durability required to secure our 2-year ambient shelf life under extreme theater heat.

Ensuring Operational Readiness through Precision Manufacturing
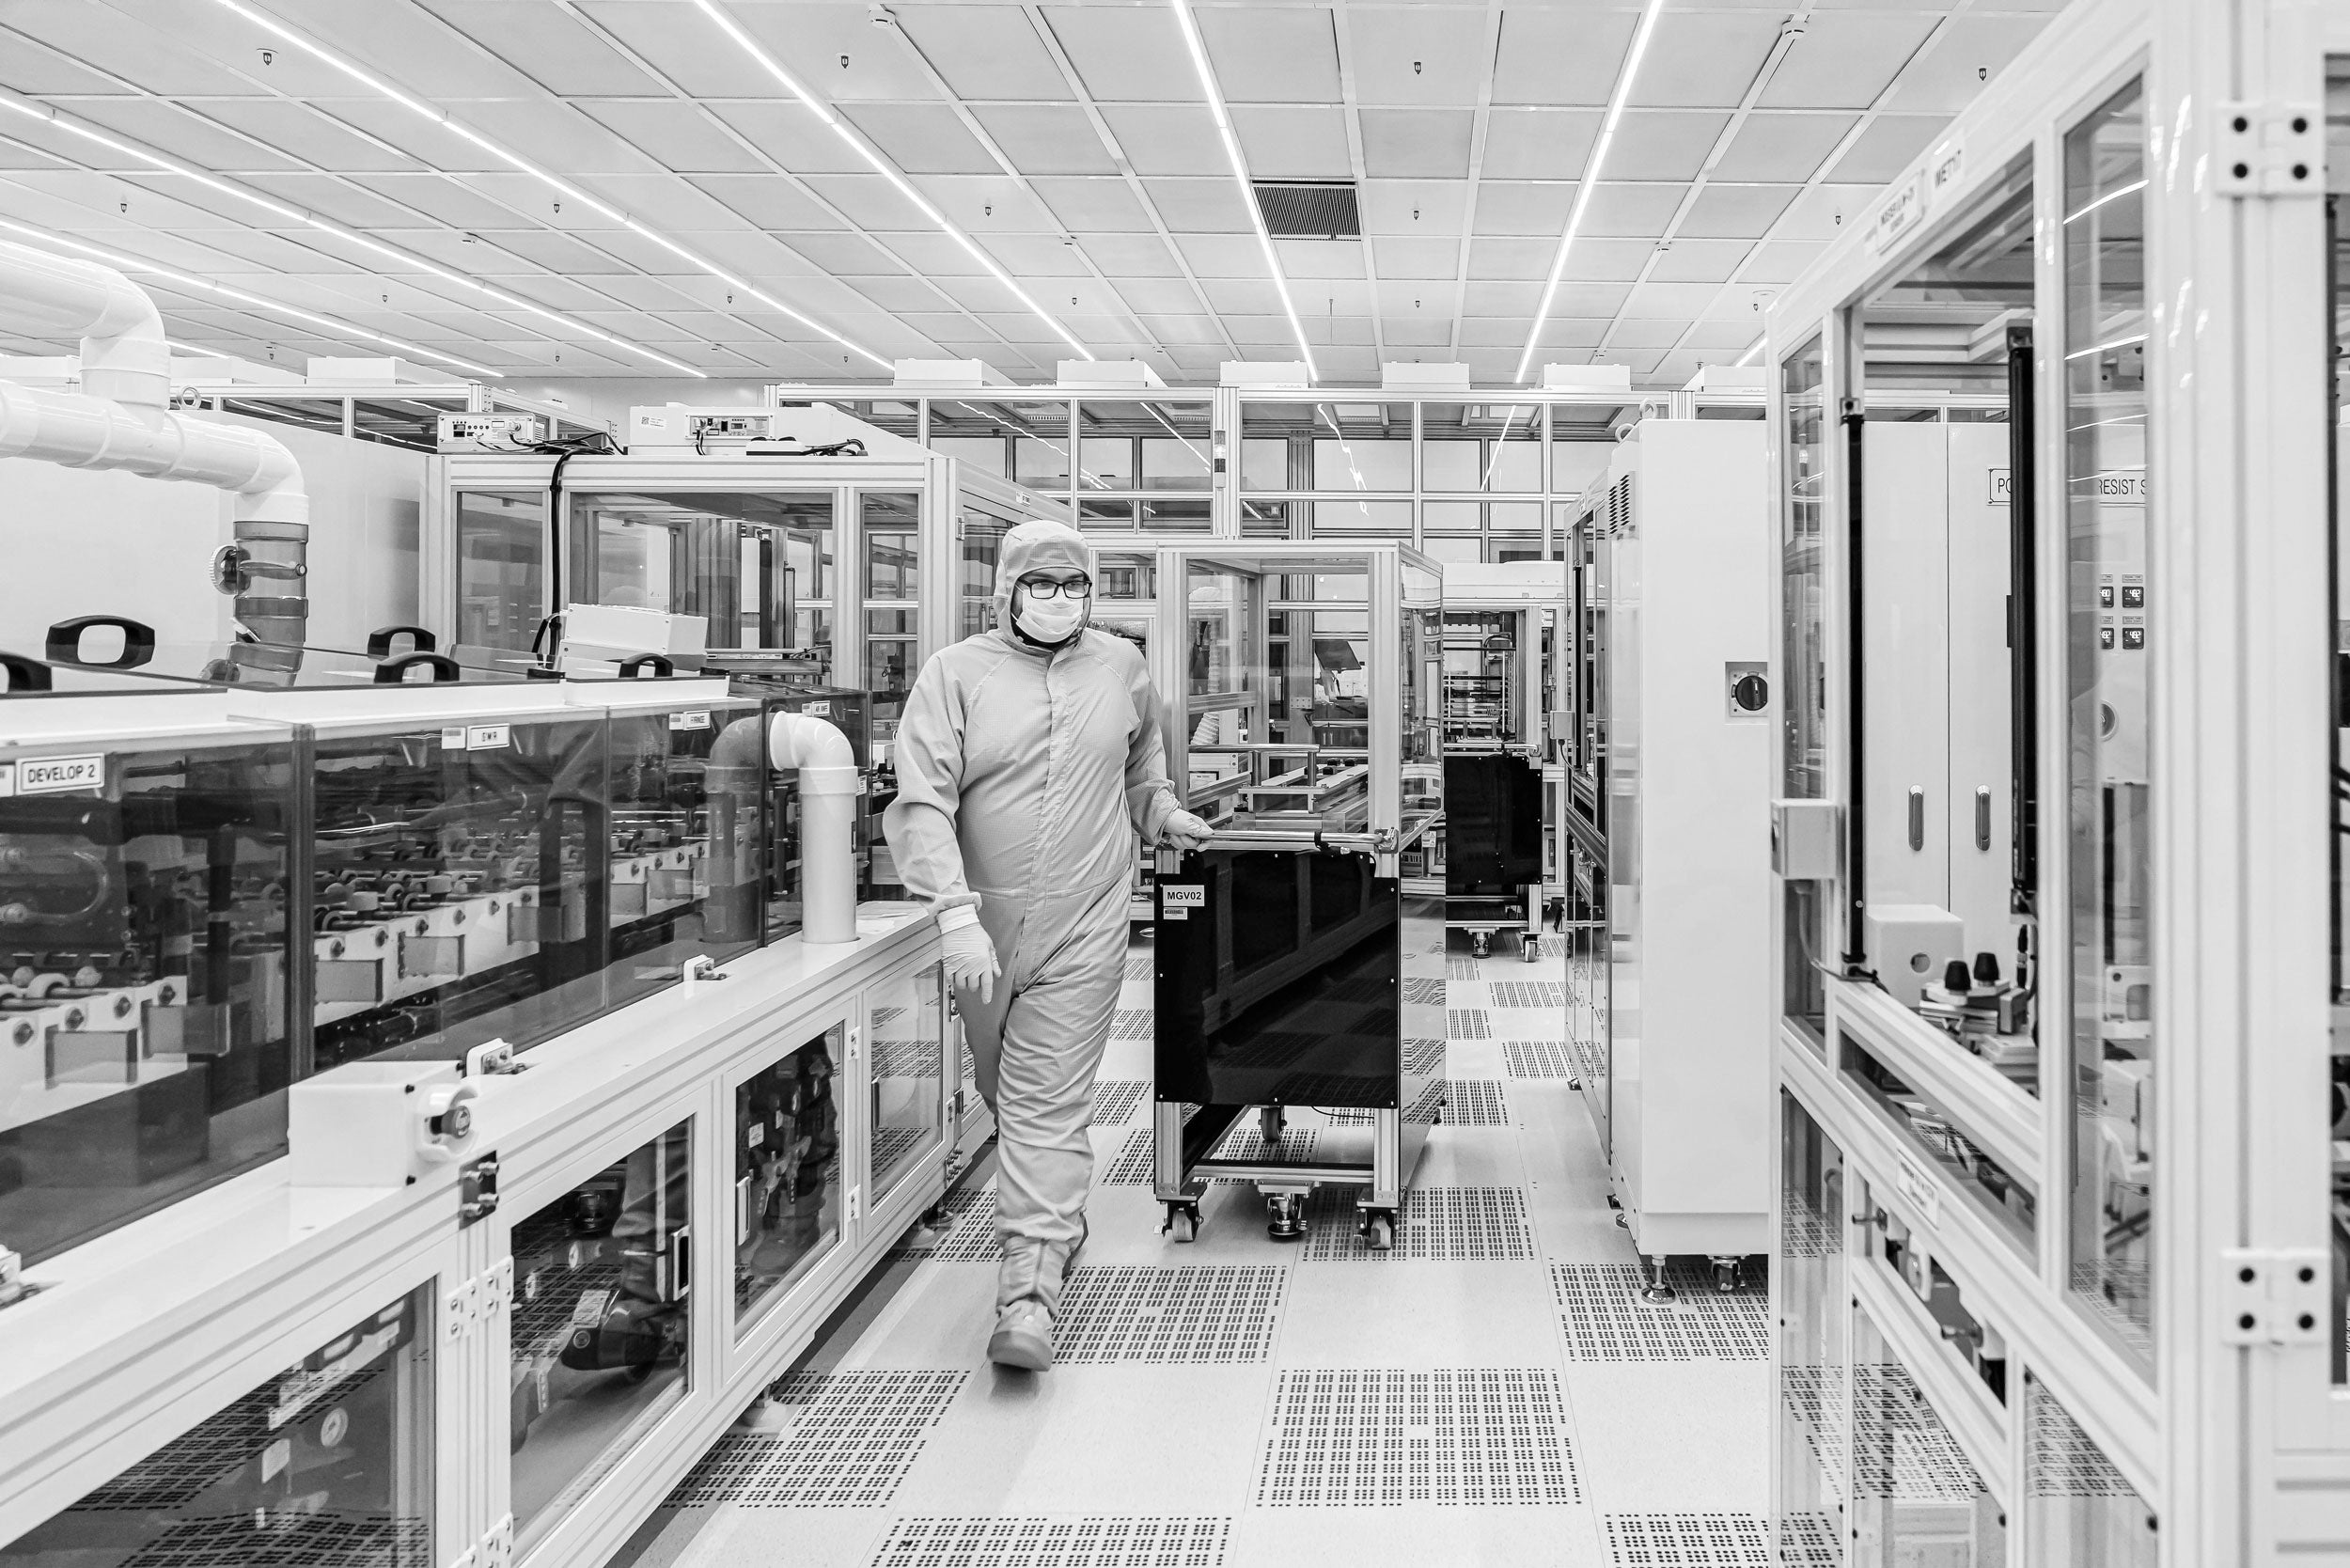
I am on-site directly at our high-speed sachet production facility, where our operating rule is absolute: Zero Deviation. At Blackstone Group OPS, we do not run a standard food commercial plant. We engineer tactical-grade physiological infrastructure built to sustain human performance in the most demanding environments on Earth. Supplying the U.S. military and our NATO allies requires far more than just filling out a standard compliance form — it demands a strict culture of unyielding hygiene, industrial security, and mass-volume execution.Our specialized automated infrastructure delivers complete material certainty:
- Absolute Batch Traceability: Every individual sachet that leaves our automated production line is tracked lot-to-lot and batch-to-batch.
- GMP-Certified Frameworks: Continuous manufacturing runs operate under strict, medical-grade clean-room protocols.
- Total Supply Security: This rigorous oversight guarantees 100 percent material integrity before the product ever hits a transit warehouse.
- The Mission-Ready Standard: Excellence is our daily operating procedure to ensure full force preservation.
- Preventative Material Protection: We build our lines to protect your ground personnel from bodily breakdown so they can stay focused entirely on the mission.